Electrostatic Coating Equipment Manufacturer · Sample Spray Testing AvailableSales & Support:151-1863-0086
Get a QuoteTechnical Resources中文
Home/Industry Solutions/Auto Parts Coating
Auto Parts

Auto Parts Coating

Requirements for film thickness consistency and batch stability are far higher than for ordinary industrial parts.

Typical Working Conditions in This Industry

Auto parts (subframes, brackets, chassis parts, wheel hubs, battery trays) are characterized by:

  • Clear standards for film thickness and adhesion, not “looks about right”
  • Complex structures, with many welded positions, internal cavities and reinforcing ribs
  • Large batches with stable batch-to-batch output; any fluctuation will be caught by sampling inspection
  • Frequent need to meet OEM process capability (Cpk) requirements

Three Levers for Film Thickness Consistency

Variable Control method
Gun travel speed Locked into the reciprocator program; not judged by eye
Powder output Centralized powder feed + stable fluidizing air pressure; powder level not below the lower limit
Gun distance Fixed gun frame or program control, profiling the workpiece shape

Once these three are stable, the remaining in-batch variation comes mainly from powder batch differences and pretreatment quality fluctuation.

Coverage of Complex Structural Parts

Welded positions, internal cavities and bolt hole positions are typical coverage blind spots.

Approaches:

  1. Arrange multiple guns at multiple angles — do not expect a single gun to solve every face from the front
  2. Rotate or turn the workpiece — bring hidden faces into an angle the field can reach
  3. Pre-spray station — low-pressure pre-spray on critical internal cavity positions
  4. Check the grounding path — complex parts often contact the hanger at multiple points, and poor contact at one point causes insufficient coating over an entire area

Reclaimed Powder Blending

The reclaimed powder blend ratio is the balance point between cost and quality.

Recommendations:

  • Keep the blend ratio at 20–30%, and it must be sieved to remove caking and contamination
  • Do not blend across color families; do not use material blended with dark reclaimed powder for light-colored parts
  • For critical appearance parts, use fresh powder; use reclaimed powder for non-appearance parts
  • Record the blend ratio for each batch so quality fluctuations can be traced back

Locking In Parameters at Batch Number Changes

Color deviation or a change in transfer efficiency after a powder batch number change is a common complaint.

Suggested procedure:

  1. On arrival of a new batch number, do a small-sample trial spray and compare color panels and film thickness with the previous batch
  2. Record the optimum voltage, air pressure and gun distance parameters for that batch number
  3. Build a batch parameter log so the same batch number can be called up directly next time
  4. If parameter changes exceed the range, contact the powder supplier to confirm the batch difference

What We Need From You

  • Workpiece drawings or physical photos (marking critical coverage positions)
  • Target film thickness range and adhesion standard
  • Hanger type and number of pieces hung per hook
  • Daily output and existing conveyor line speed
  • Whether OEM audit requirements apply (e.g. Cpk, PPAP)

The Most Common Problems in This Industry

Film thickness varies widely between workpieces in the same batch, causing failed customer sampling inspection

Internal cavities and welded positions on complex structural parts are hard to cover

High powder consumption per unit, and the reclaimed powder blend ratio is difficult to get right

Process parameters must be worked out again after a batch number change, causing large trial production losses

Recommended Configuration

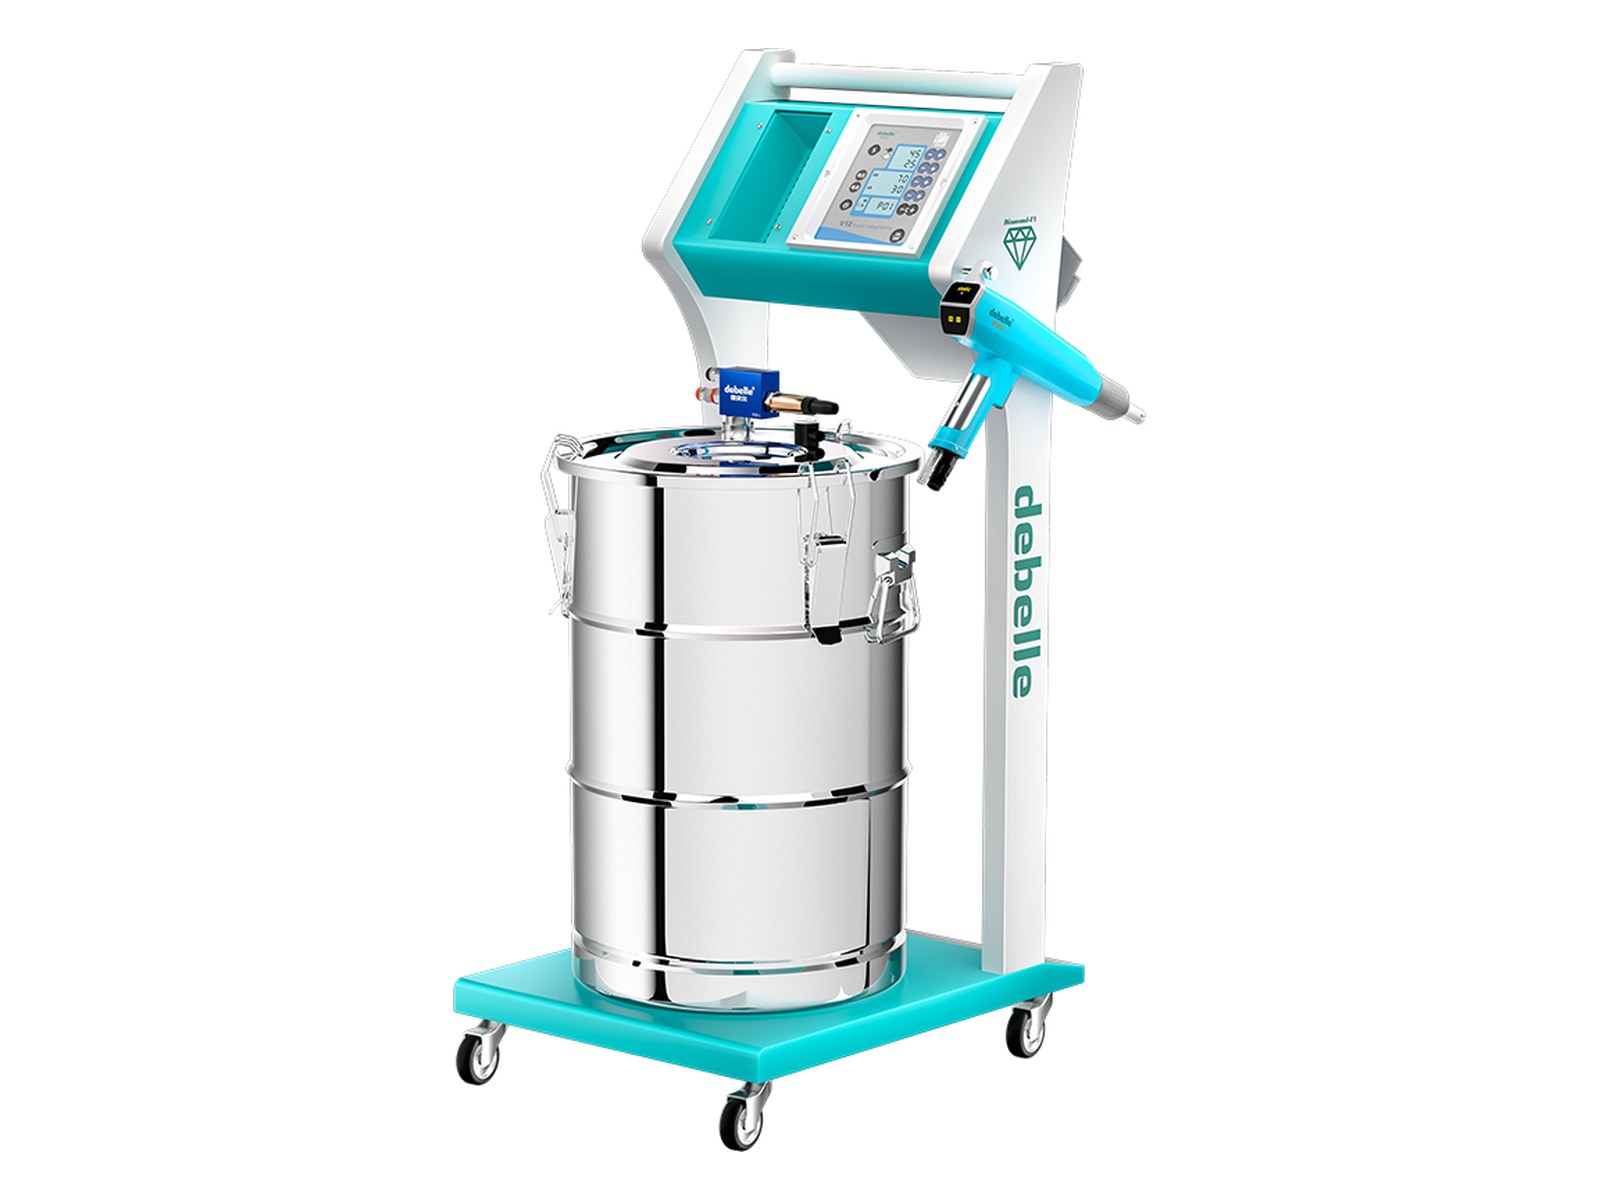
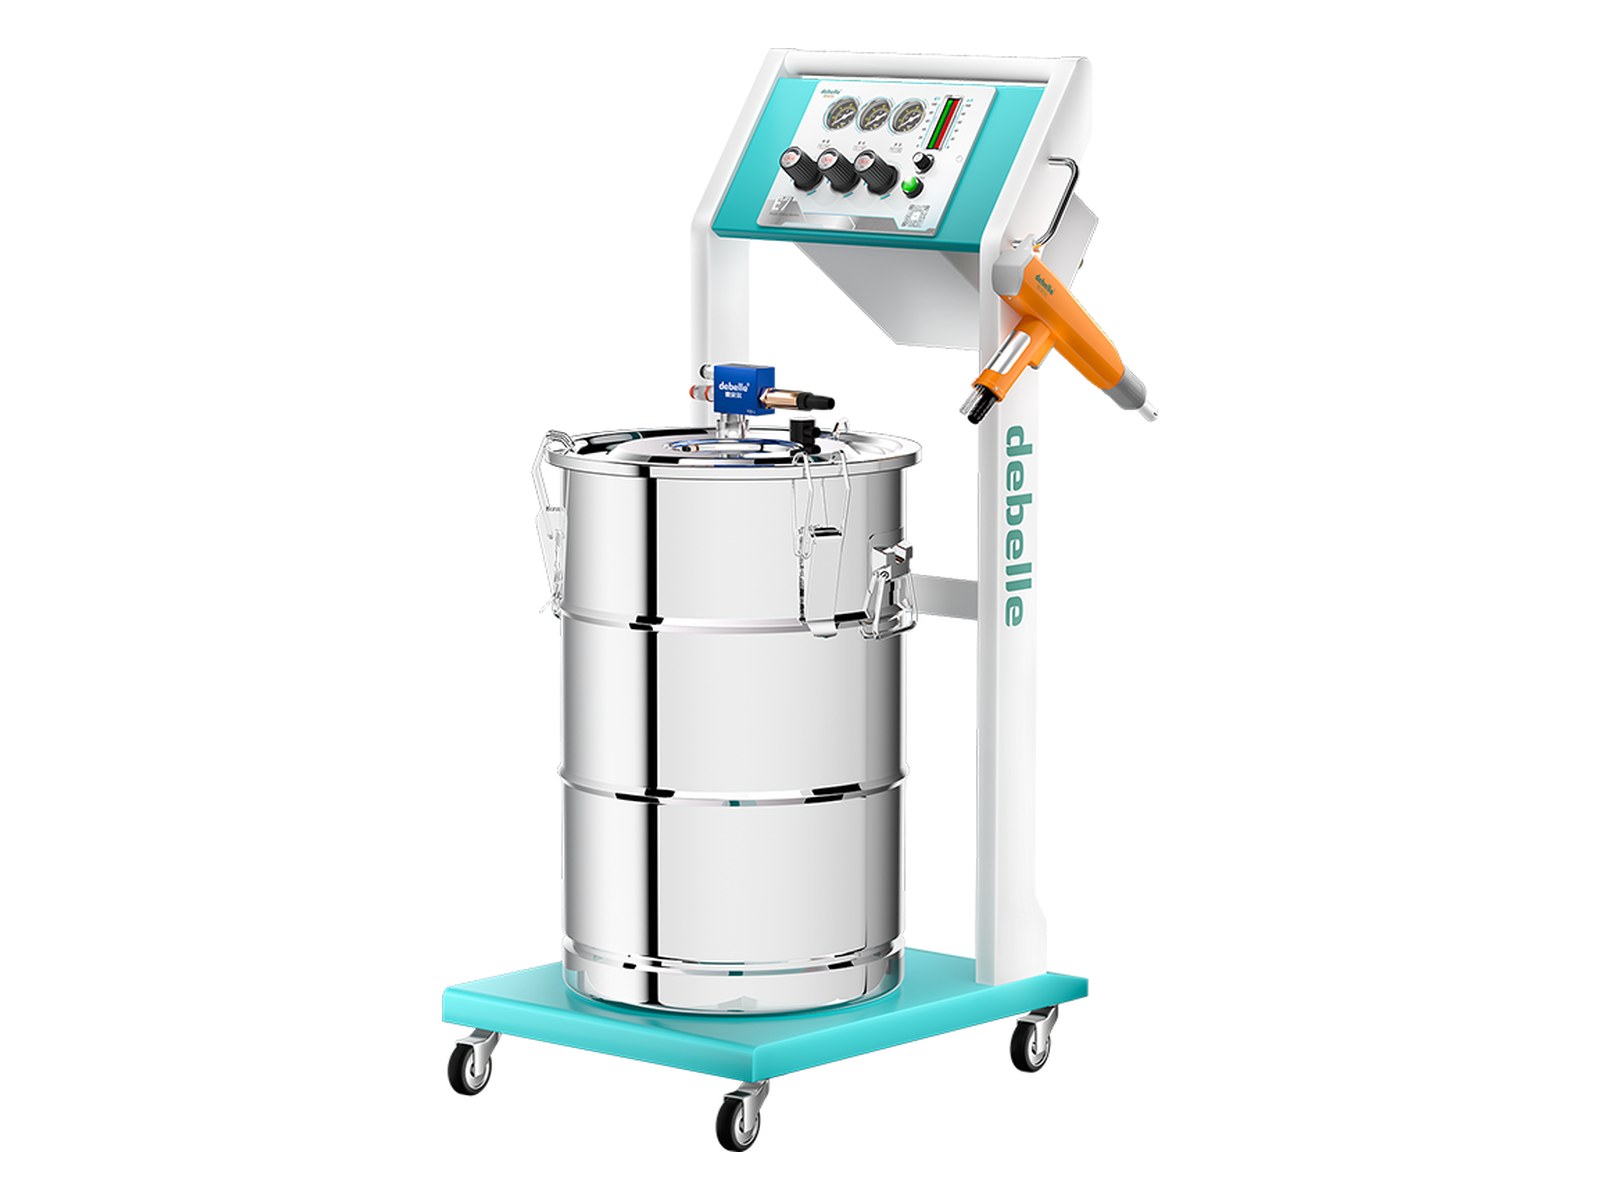
E7 Manual Electrostatic Powder Coating Gun E7
ManualE7

E7 Manual Electrostatic Powder Coating Gun

DEBELLE's classic entry-level manual electrostatic powder coating gun with adjustable 0-85kV output and automatic voltage tracking by gun distance. A cost-effective choice for flat panels and small-to-medium batches.

View details →
E7 Automatic Electrostatic Powder Coating Gun E7
AutomaticE7

E7 Automatic Electrostatic Powder Coating Gun

Automatic version sharing the same control unit as the E7 manual gun, ideal for conveyor-line batch coating with a reciprocator. Control unit is reusable, keeping upgrade costs low.

View details →
V12 Manual Electrostatic Powder Coating Gun V12
ManualV12

V12 Manual Electrostatic Powder Coating Gun

The all-round CNC machine, all in one step: 0-100kV with LCD display, 20 main programs + over 500 sub-programs storage, one-touch gun purge — covering all the capabilities of the E7 and 960.

View details →
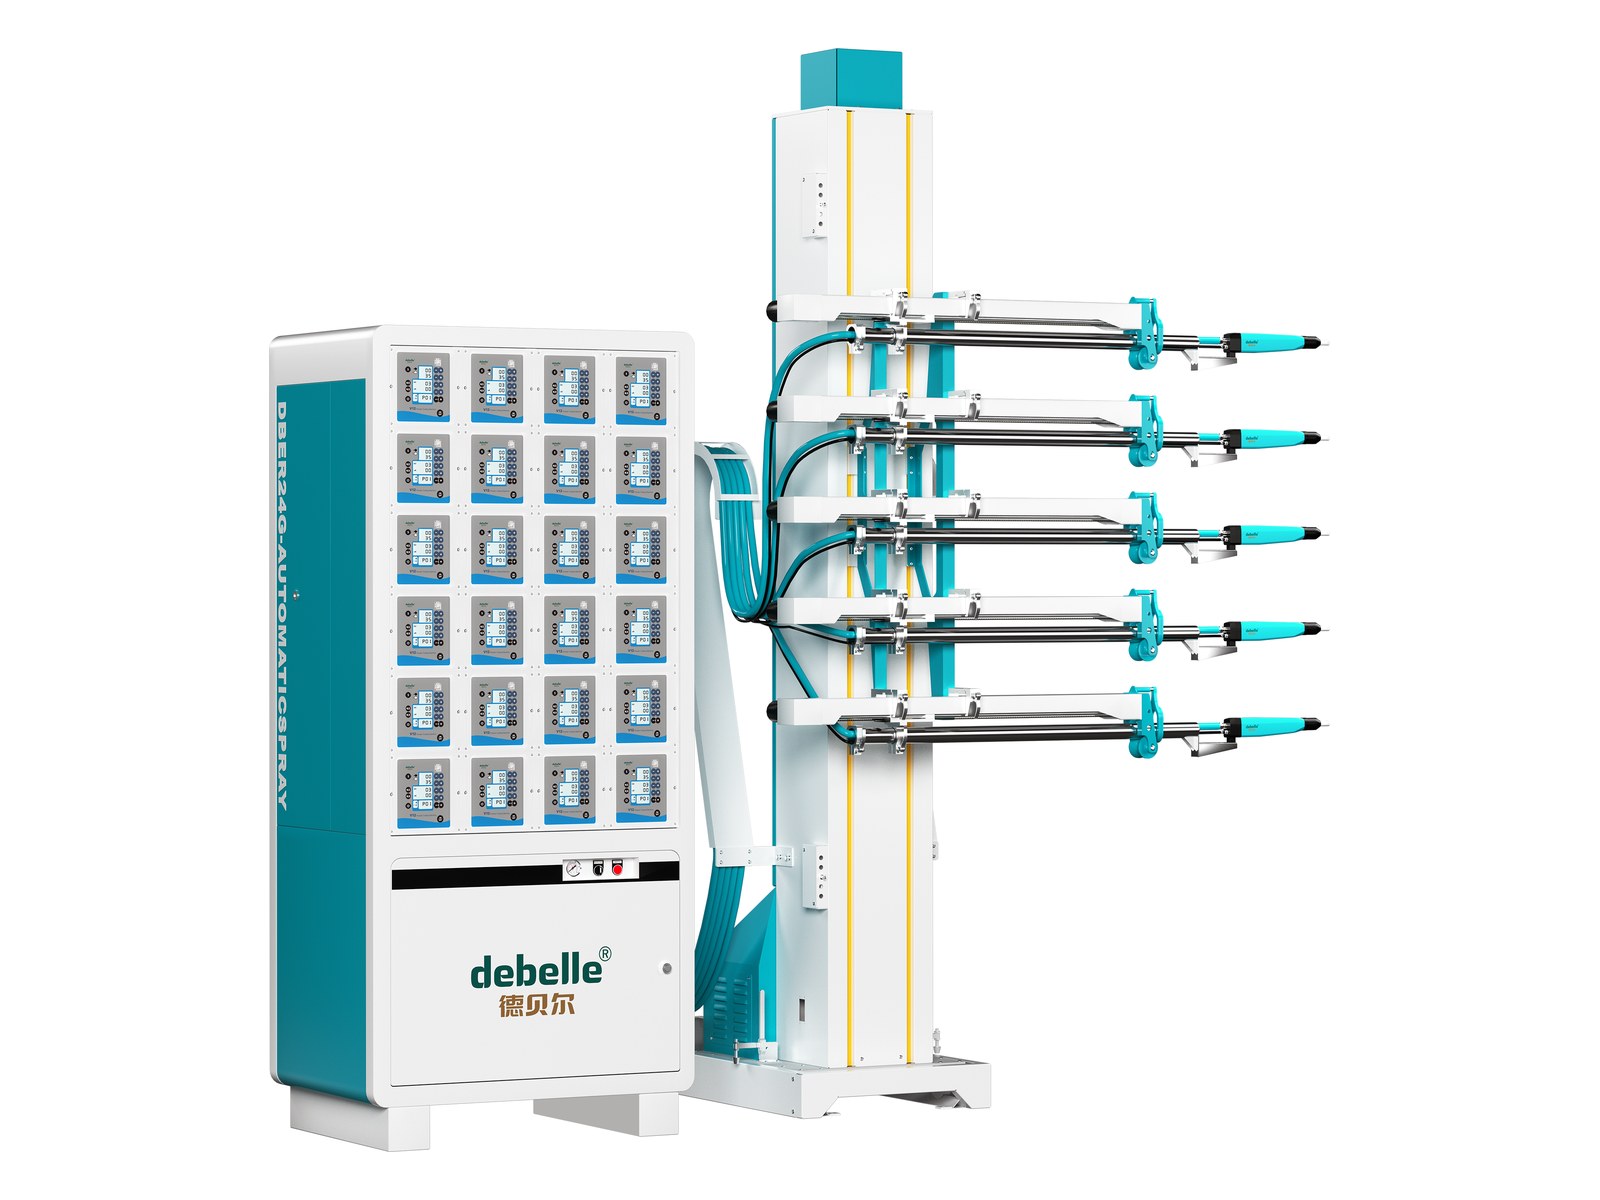
V12 Automatic Electrostatic Powder Coating Gun V12
AutomaticV12

V12 Automatic Electrostatic Powder Coating Gun

CNC automatic flagship with one-touch gun purge, multi-gun interlock control, and cross-backup control units that keep production running — the core solution for large powder booth automatic lines.

View details →

Need a Proposal for Your Workpieces?

Provide workpiece dimensions, material, daily output and powder model — we deliver a selection proposal and configuration list.

Get a Proposal
CallGet a QuoteWhatsAppTop